The food industry relies on reliable, compliant lubricants and gear solutions to keep processing lines, conveyors, and machinery operating smoothly. This guide highlights five top products that meet food-safety standards and perform under demanding environments—from freezing temperatures to high-load gear systems. Each option emphasizes NSF H1 certification, water resistance, and temperature resilience to help prevent contamination and downtime in meat, dairy, beverage, and confectionery operations.
| Product | Brand |
|---|---|
| BX-434 NSF H1 Food Grade Plastic Grease 14.1oz | LewisCare |
| Chef Collection Food-Safe Gear Lubricant, 1 Gallon | Chef Collection |
| Multi-Purpose Food Grade Grease 14.1oz 2 Pack | LewisCare |
| BX-303 FM Food Grade Grease NSF H1 White Lithium | LewisCare |
| BX Food Grade Grease 2.8 oz 2 Pack | LewisCare |
Choosing the right lubricant for food machinery involves understanding NSF H1 certification, temperature range, water resistance, and the compatibility with bearings, gears, and seals. The products below are selected for versatility across ice cream machines, conveyors, mixers, gear trains, and processing lines while maintaining food safety standards and ease of maintenance.
BX-434 NSF H1 Food Grade Grease — Low-Temperature to High-Temp Performance

This 14.1-ounce grease from LewisCare is NSF H1 certified for incidental food contact, making it suitable for meat processing, dairy, beverage production, and cold drink lines. It is designed for industrial applications, protecting bearings, gears, and chains in high-demand equipment such as conveyors, mixers, and fillers, including ice cream machinery. Its cold-ready performance supports smooth operation from -15°C to 100°C, helping ensure continuity in frozen product lines and chilled beverage systems.
Key considerations include compatibility with plastic components and a focus on maintaining lubrication while minimizing contamination risk. The formulation aims to deliver reliable wear protection and reduced moisture-related degradation, which is critical for long-running food processing equipment in cold environments.
Chef Collection Gear Lubricant — Food-Safe Industrial Gear Oil

This 1-gallon gear lubricant is designed for industrial use while being safe for contact with processing machinery. It provides robust lubrication for gears and gear trains, reducing wear and improving efficiency in food processing environments. The product is formulated to minimize contamination risk and maintain equipment reliability across long runs in manufacturing facilities.
Considerations include ensuring proper viscosity for gear systems, compatibility with seals and plastics, and minimizing any residual odor or color that could affect food environments. Regular inspection and routine lubrication intervals are recommended to maximize uptime and protect complex gear assemblies in production lines.
Multi-Purpose Food Grade Grease 14.1oz 2 Pack

This LewisCare 14.1-ounce, 2-pack provides food-grade lubrication ideal for bearings and components within food machinery. The grease is formulated to meet strict safety and regulatory standards for incidental contact with food products, offering high-performance lubrication for various machine components. It aims to reduce friction, wear, and extend service life in demanding processing environments.
Key advantages include food-grade purity, water resistance, and stable performance across a wide temperature range. In practice, users should verify compatibility with specific seals and chassis materials and schedule periodic reapplication to maintain consistent protection across the equipment fleet.
BX-303 FM Food Grade Grease — White Lithium, NSF H1
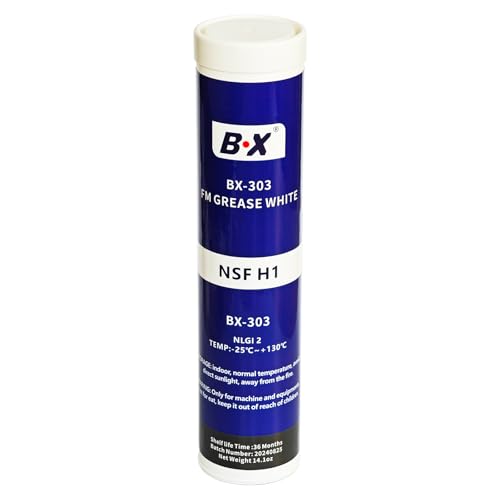
BX-303 FM is a white lithium grease with NSF H1 certification, designed for food machinery and bearing lubrication in commercial kitchens and processing plants. The formula is colorless and odorless to minimize contamination risk and supports smooth operation for extended periods. It is positioned for reliability in gear boxes and moving parts requiring steady lubrication.
Considerations include ensuring alignment with facility maintenance schedules, inspecting for compatibility with metal and plastic components, and monitoring for any changes in viscosity due to temperature fluctuations in processing lines.
BX Food Grade Grease 2.8 oz — Water-Resistant Lubricant

This compact 2-pack provides a water-resistant, NSF H1-certified grease suitable for ice cream machines, kitchen appliances, plumbing valves, and O-rings. Its oil-free, low-temperature performance enables reliable starting and operation from -15°C to 100°C, making it a versatile option for mixed-use environments where moisture exposure is common.
Purchase considerations include the applicability to small fittings and seals, ensuring proper pump or nozzle compatibility, and maintaining clean handling practices to prevent cross-contamination within food processing areas.
Buying Guide: Key Purchase Considerations for Food Industry Lubricants
- Certification and Safety: Prioritize NSF H1 or equivalent certifications to ensure incidental contact with food is safe. Confirm any regulatory requirements for your region and sector (dairy, meat, beverages, bakery, etc.).
- Temperature Range: Match the lubricant’s operating temperature with your equipment’s thermal profile. Cold-start performance matters in freezers and ice cream lines, while high-temperature stability matters in cooking or overheated gear systems.
- Water Resistance: In wet environments or cleaning cycles, water resistance reduces washout and corrosion. Look for formulations designed to resist moisture and frequent washdowns.
- Material Compatibility: Check compatibility with plastics, rubbers, seals, and metal surfaces in your machinery. Inadequate compatibility can cause swelling, leakage, or seal damage.
- Gear and Bearing Needs: Select lubricants based on lubrication points—bearings, gears, chains, or o-rings. Some products are multipurpose, while others are specialized for gear trains or chains.
- Viscosity and Load: Consider load-carrying capacity (NLGI grade) and viscosity to ensure endurance under heavy-duty operation and high-speed conditions without thinning or separation.
- Food Safety and Odor: Choose clear, odorless formulations where possible to prevent contamination signals or odor transfer in sensitive environments like bakeries or dairy lines.
- Maintenance and Re-application: Evaluate re-lubrication intervals and ease of application. Greases with longer service life reduce downtime and maintenance costs.
- Packaging and Storage: Smaller tubes for tight spaces, larger gallons for centralized systems, and proper storage to prevent contamination or degradation.
- Vendor Support: Prefer brands with readily available technical data, compatibility charts, and reliable customer support to tailor solutions to your process.
Across these options, the goal is to maintain equipment reliability, ensure food safety, and minimize downtime in demanding processing environments. When in doubt, consult equipment manuals and reach out to lubricant manufacturers for precise recommendations based on your facility’s equipment list and operating conditions.