Choosing the right grease for food processing equipment is essential for safety, uptime, and compliance. The following selections are NSF H1 or equivalent, suitable for incidental contact with food, and designed to withstand the rigors of mixers, conveyors, grinders, and beverage lines. This guide compares options across temperature ranges, thickening systems, and application types to help facilities pick the best fit for their operations.
| Product | Brand | NSF/Certifications | Key Use |
|---|---|---|---|
| Petrol-Gel Food Grade Equipment Lubricant | Petrol-Gel | NSF Approved | General food processing equipment |
| BX-434 NSF H1 Food Grade Plastic Grease | LewisCare | NSF H1 Certified | Bearings, gears, conveyors |
| Sta-Lube Multi-Purpose Food Grade Grease SL35600 | CRC | NSF H1 | Multi-purpose, wide temp range |
| Keze Food Grade Equipment Lubricant | Keze | NSF H1 Registered | Kitchen and beverage equipment |
| Verdana Food Grade Lubricant Oil | Verdana | NSF H1 | Meat slicers, grinders, non-petroleum oil substitutes |
These options cover a spectrum of needs—from light-duty, high-cleanliness environments to heavy-duty bearings and cold lines. They are designed to minimize contamination risk, extend equipment life, and maintain consistent performance in busy food processing settings.
Petrol-Gel Food Grade Equipment Lubricant

Petrol-Gel offers an NSF-approved mineral oil-based lubricant intended for food processing equipment. It is formulated to minimize friction and wear on moving parts, helping extend component life in mixers, meat grinders, and other culinary machinery. The product emphasizes food safety, ensuring that any incidental contact with foods remains free from harmful contaminants. Its design supports reliable operation in environments where routine lubrication is essential for smooth production lines.
BX-434 NSF H1 Food Grade Plastic Grease

LewisCare’s BX-434 is an NSF H1 certified grease designed for industrial food processing equipment. It protects bearings, gears, and chains in conveyors, mixers, fillers, and cold-drink/ice-cream machinery. The cold-ready performance allows operation from -15°C to 100°C, which is beneficial for frozen product lines and chilled beverage systems. The grease’s formulation supports high-demand applications, maintaining viscosity and lubrication under rapid temperature shifts common in food processing plants.
Sta-Lube Multi-Purpose Food Grade Grease SL35600
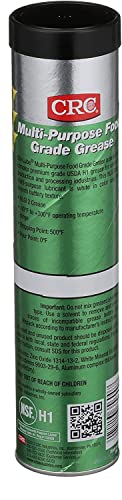
Sta-Lube SL35600 is a premium NLGI Grade 2 aluminum complex grease with NSF H1 registration. Its white composition provides visible cleanliness in food processing environments, and the formulation emphasizes water resistance and a broad operating temperature range. This multipurpose grease is suitable for gearboxes, bearings, and other moving parts in kitchens and processing plants, offering a balance between film strength and washout resistance crucial for high-demand operations.
Keze Food Grade Equipment Lubricant

Keze offers a 2-pack of NSF H1 registered, odorless grease tailored for kitchen equipment and beverage systems. Its compatibility with stand mixers, slushie machines, espresso gear, and other processing equipment makes it a versatile choice for facilities with diverse machines. The grease reduces friction and gear wear, contributing to longer service life of grinders, seals, and O-rings while maintaining food safety standards in incidental contact scenarios.
Verdana Food Grade Lubricant Oil
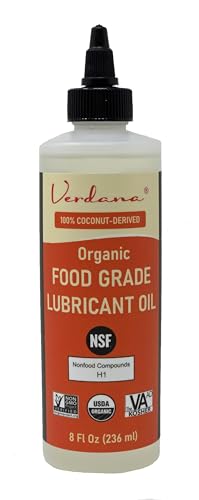
Verdana’s food-grade lubricant oil is NSF H1 certified and petroleum-free, offering a clean alternative for meat slicers, grinders, and other food-contact equipment. Made from organic, coconut-derived ingredients, it avoids petroleum and GMOs while delivering lubrication needs. The product also serves as a rust and corrosion inhibitor, contributing to equipment longevity in moist or high-humidity environments typical of food processing facilities.
Buying Guide: Key Purchase Considerations
When selecting a grease for food processing equipment, several factors determine long-term performance and safety:
- Regulatory certification: Prioritize NSF H1 or equivalent approvals to guarantee incidental food contact safety and regulatory compliance. Check whether the product carries additional certifications relevant to your region or industry.
- Base oil and thickener: Mineral oil-based vs. synthetic, and thickeners such as lithium, aluminum complex, or polyurea influence temperature range, wear protection, and water resistance. This choice affects suitability for warm kitchens or cold beverage lines.
- Temperature range: Identify operating temperatures of your equipment. Cold lines and freezers require grease with low-temperature performance; high-heat equipment benefits from high dropping points and stable viscosity at elevated temperatures.
- Water resistance and washout: Food plants often operate in humid or washdown environments. Choose greases with strong water resistance to prevent grease washout and thinned lubricants during cleaning cycles.
- Equipment compatibility: Consider whether the grease is formulated for bearings, gears, chains, O-rings, or seals. Some products are multi-purpose, while others target specific components.
- Viscosity and film strength: The right viscosity ensures adequate lubrication without oozing or attracting debris. A higher film strength helps protect moving parts under heavy loads.
- Odor and cleanliness: In culinary settings, odorless formulas reduce contamination risk and improve working conditions, particularly in food prep areas or cold storage.
- Packaging and quantity: Larger batches can reduce downtime for maintenance, but storage and shelf life matter. Ensure packaging is suitable for your maintenance cadence and storage space.
- Applications and use case: Some greases are ideal for ice cream equipment, others for meat processing lines. Match the product to your specific machines and operating conditions.
- Regulatory hygiene and sanitation: For facilities with strict cleaning schedules, consider greases that tolerate frequent washdowns and do not degrade under sanitizers.
In practice, a facility may adopt a mix: a general-purpose NSF H1 grease for conveyors and mixers, a specialized cold-weather grease for ice cream lines, and a premium aluminum complex grease for high-load gearboxes. Always document lubricant specifications, maintenance intervals, and equipment compatibility to optimize uptime and safety.